How to Determine When Twin Screw Extruder Components Need to Be Replaced
Nov 13, 2026
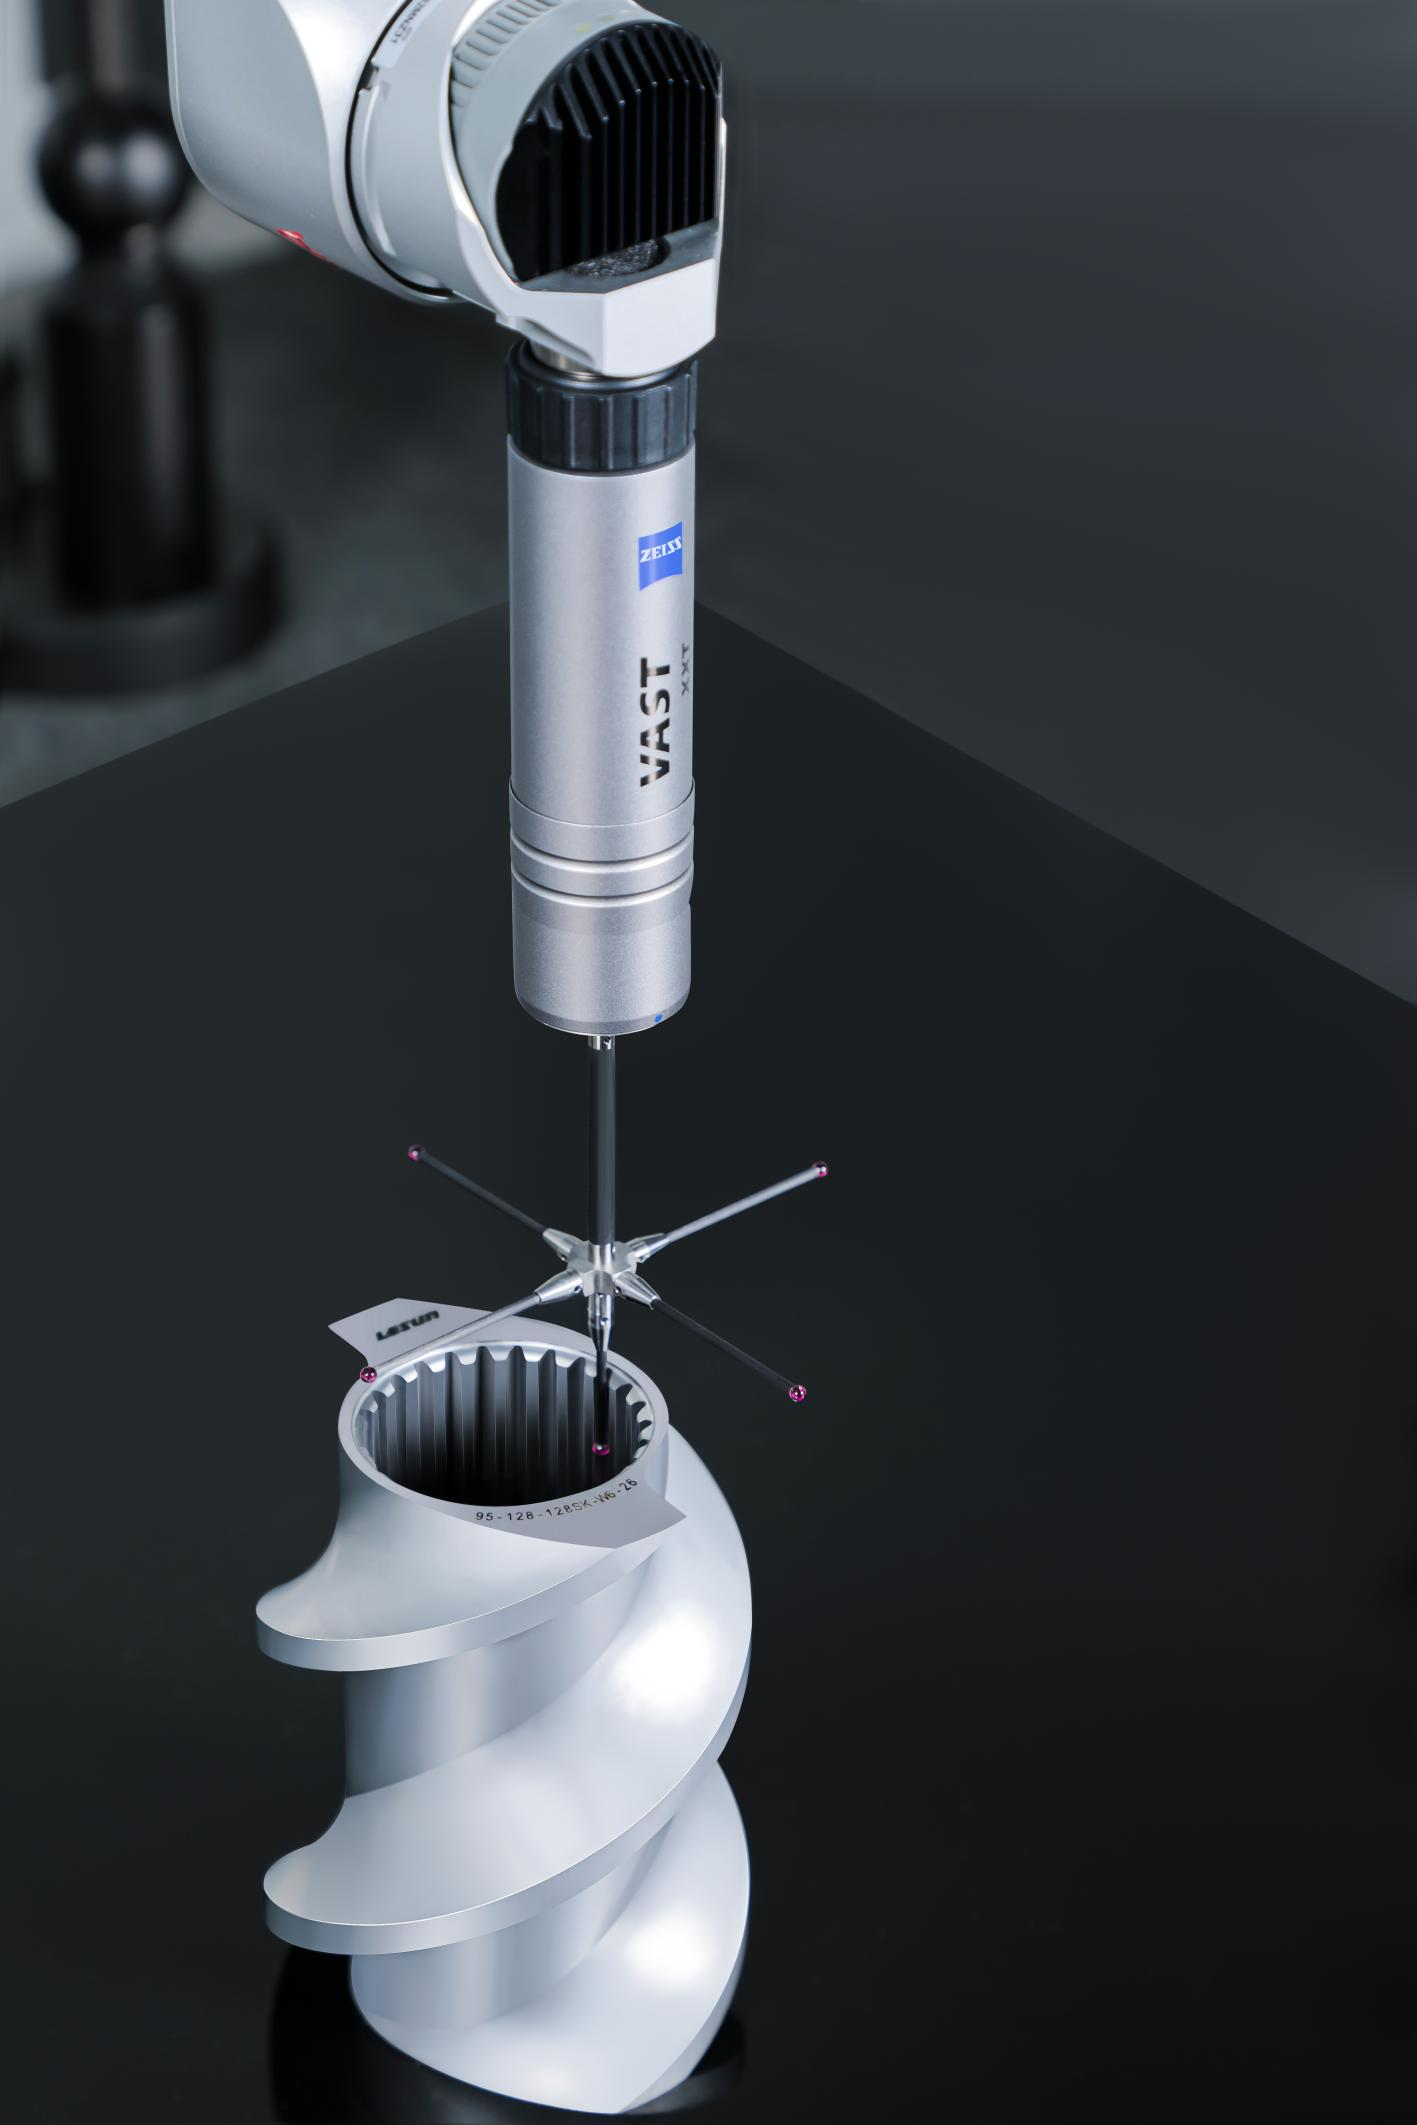
Nanjing, Jiangsu Nov 12, 2026 (Issuewire.com) - How to Determine When Twin Screw Extruder Components Need to Be Replaced Balancing Component Life and Production Requirements Replace or repair twin-screw extruder components when measured wear reaches the applicable service limit, confirmed wear prevents acceptable production, or physical damage makes continued operation unacceptable. Start planning before that point so that replacement parts arrive in time for a scheduled shutdown. This guide focuses on modular, co-rotating twin-screw extruders used in polymer compounding. Screw elements, kneading blocks, barrels and drive shafts need different acceptance criteria. There is no single operating-hour interval, percentage of diameter loss or backlash angle that reliably determines replacement for every machine. A useful maintenance decision combines dimensional measurements with product quality and process trends. Continued service may be reasonable while dimensions remain acceptable and production is stable. Conversely, a component may need replacement before its dimensional limit if confirmed wear causes unacceptable dispersion, contamination or loss of operating capacity. The framework below provides practical decision guidance; machine-specific limits remain the responsibility of the equipment manufacturer or a qualified engineering assessment. Linking Process Symptoms to Wear Inspections Establish a baseline with serviceable components. Record the formulation, actual feed rate, screw speed, melt temperature, pressure measurement location, drive torque or load, and relevant product-quality results. Compare like-for-like runs and first check feeding, temperature control, downstream restrictions and instruments before attributing an anomaly to wear. Declining Conveying or Pressure Building Performance Wear of flight tips and barrel bores increases clearance. In melt-filled pressure-building sections, increased leakage can reduce pumping efficiency. Inspect both the screw elements and their mating barrel sections when performance progressively deteriorates. A sudden change also calls for investigation of feed interruptions, blockages or acute damage. On a starve-fed twin-screw extruder, throughput is primarily controlled by the feeder; unchanged output does not prove that the screws remain unworn. When to replace: Repair or replace the affected components when their measured geometry reaches the applicable service limit, or when confirmed wear prevents the required output and pressure from being maintained within the approved process window. Check barrel dimensions before fitting new elements so that the replacement actually restores an acceptable clearance. Deteriorating Dispersion or Blend Uniformity Inspect kneading blocks and mixing elements (https://www.lesunscrew.com/products/mixing-screw-elements/)when pigment dispersion, filler agglomerate levels or blend uniformity deteriorate under comparable conditions. Wear can change local stresses and material flow. Temperature spikes alone do not identify worn mixers, and increased clearance does not necessarily increase viscous heating. Dispersive mixing breaks agglomerates; distributive mixing spreads ingredients through the melt, so the inspection should reflect the function of each element. When to replace: Replace elements with out-of-limit profiles or clearances, or when confirmed wear prevents the product from meeting its mixing specification after other process causes have been addressed. Use the product's established dispersion or uniformity test rather than visual impressions alone. Recurring Contamination or Fluctuating Drive Load Pitted or damaged surfaces can retain polymer that later degrades and contaminates the product. Recurring black specks therefore justify inspecting barrels and other possible retention sites, including downstream adapters and dies. Motor-current or torque fluctuations are less specific: they indicate changing load and require a broader check of feeding, melting and the drivetrain. They do not independently establish barrel damage. [7, 8] When to replace: Repair, reline or replace a barrel section if it exceeds its dimensional limit or is confirmed as a persistent contamination source that cleaning cannot resolve. Select the option according to the barrel construction and the condition of its housing and liner. A visible scratch alone is not an automatic replacement criterion. Increasing Vibration or Rotational Play Inspect bearings, gears, couplings, alignment and spline interfaces when vibration, impact noise or rotational play increases. Localize the movement before attributing it to a screw shaft; backlash measured through the entire drivetrain includes several interfaces. Misalignment can also produce additional drive load and premature screw and barrel wear. When to replace: Replace or obtain an approved repair for a shaft or mating spline component when its fit exceeds the applicable limit or tooth damage compromises torque transmission. Inspect internal and external splines together. Cracks, broken teeth, spalling or confirmed mechanical interference warrant shutdown and engineering assessment before further operation. Quantitative Criteria for Replacement Decisions Measure the Relevant Geometry Obtain the original dimensions, tolerances and service limits for the exact machine and component. Record whether a clearance is radial or diametral: for a concentric screw flight envelope and barrel bore, radial clearance is half the difference between bore diameter and flight outside diameter. These values must not be compared interchangeably. Twin-screw assemblies also require assessment of intermeshing profiles and screw-to-screw clearances using the manufacturer's method. The critical measurement is the local condition at the relevant location, not an average across the whole assembly. Record flight dimensions at repeatable positions, inspect kneading-disc profiles, and map barrel wear in both bores and the intermeshing region. Coperion's inspection approach combines barrel measurements with surface inspection to identify wear and damage. If no service limit is available, obtain a component-specific engineering assessment. Decide Whether to Monitor or Replace Condition Recommended action Measurements remain within limits, trends are stable and product requirements are met Continue service and retain a scheduled inspection interval. Wear is progressing toward a limit or repeatable performance deterioration is emerging Shorten the inspection interval, investigate the cause and prepare replacement parts. A service limit is reached, or confirmed wear prevents acceptable production Schedule replacement or approved repair; do not assume continued operation is acceptable without assessment. Cracking, broken teeth, spalling or mechanical interference is found Stop operation and determine the damage and repair scope before restarting. This decision framework distinguishes early planning from component rejection. Davis-Standard likewise separates closer monitoring and replacement preparation from the higher wear level at which rebuilding or replacement is recommended, while noting that individual applications vary. Its feedscrew figures should not be transferred directly to modular twin-screw components. Use Wear Trends to Plan the Shutdown Estimate the rate of change from repeated measurements at the same location and under comparable measurement conditions. For an increasing clearance, a simple planning calculation is the remaining margin to the approved limit divided by the recent rate of clearance growth. Illustrative calculation only: If a measured clearance increases from 0.20 mm to 0.26 mm over 2,000 operating hours, its average growth is 0.03 mm per 1,000 hours. If 0.32 mm were the approved limit for that particular location, linear extrapolation would suggest about 2,000 additional hours to the limit. These figures are hypothetical and are not recommended twin-screw clearances. Arrange the intervention earlier than the extrapolated limit, allowing for measurement uncertainty, possible wear acceleration, procurement and installation time. Recalculate after changes in formulation, filler loading or operating conditions. Begin ordering when the conservative remaining service window approaches the time needed to obtain and install the parts. Do not use this calculation to predict the life of cracked or acutely damaged components. Component Failure Mechanisms in Polymer Compounding Abrasive fillers and reinforcements can wear screw and barrel surfaces, especially in highly loaded processing zones. Filler concentration alone does not predict service life: particle properties, screw configuration, operating conditions and component materials also matter. Inspect melting, filler-incorporation and pressure-building zones closely rather than assuming that the feed port is always the most severely worn location. Corrosion depends on the formulation and processing conditions. Moisture, reactive additives or degradation products may contribute to pitting; venting does not by itself establish that a barrel is undergoing corrosive wear. Adhesive wear or galling requires attention to contact, alignment, deflection and material compatibility. Correcting these causes is important before installing replacements. Shaft and spline deterioration can involve fretting, overload or fatigue. The manufacturing method alone does not determine failure. Cold forming can preserve grain flow and work-harden spline surfaces, but it does not eliminate backlash or make a shaft immune to fatigue. Material, heat treatment, tooth geometry, fit and operating loads must be considered together. Field Inspection and Material Verification During a planned shutdown, follow the equipment manufacturer's isolation, disassembly and cleaning procedure. Identify each element and barrel position before removal, then measure clean components at the specified reference temperature. Retain the same locations and measurement method for subsequent inspections. Use calibrated micrometers or profile equipment for suitable screw dimensions, and an appropriate bore-measurement system for barrels. A borescope identifies surface damage but does not replace dimensional measurement. Coordinate measuring machines and validated optical scanning can help assess complex profiles. Select equipment with uncertainty suitable for the tolerance being assessed; the description "sub-millimeter precision" is not sufficient to establish suitability for a small clearance. Choose nondestructive testing to match the suspected defect. Magnetic particle testing can reveal surface and near-surface discontinuities in suitable ferromagnetic shafts. Ultrasonic testing can investigate internal discontinuities where access and geometry permit. The examination method and acceptance criteria should be specified by qualified personnel; no routine test guarantees detection of every microcrack. Optical emission spectrometry checks elemental composition. It does not, by itself, establish heat-treatment quality, fatigue strength or remaining service life. Combine material certificates with appropriate hardness, metallurgical or mechanical verification when selecting replacements or investigating failures. Each inspection record should identify the component, location, measured value, applicable limit, operating hours, processed material and resulting action. Choose the next inspection interval from the observed wear rate and production risk. Tighten it after an abrasive formulation change, an overload or an unexpectedly large change in dimensions. How Lesun Screw Supports Replacement and Upgrades Nanjing Lesun Screw Co., Ltd. (https://www.lesunscrew.com/company-profile.html)supplies screw elements, barrels and shafts, with services including measurement, reverse engineering and wear-part failure analysis. Its published capabilities include coordinate measurement, a customer parts database andcold-forming technology for shafts (https://www.lesunscrew.com/how-cold-formed-screw-shafts-improve-torque-transmission-in-high-load-compounding-lines.html). These services can support identification and procurement of replacement components. Where original drawings are unavailable, a worn sample provides useful evidence, but its measured shape is not automatically the intended new-part geometry. Confirm dimensions against unworn features, mating parts, machine data and available reference components, then approve the replacement drawing before manufacture. Select materials for the actual failure mechanism. Wear-resistant tool steels, powder-metallurgy materials and suitable barrel liners may be considered for demanding applications; corrosion resistance and toughness must also match the duty. Specify grade, heat treatment and acceptance requirements for each part instead of applying one hardness range to every component. For a replacement assessment, provide the extruder model, component identification or screw layout, available drawings, inspection measurements and photographs. Include the resin and filler system, operating conditions, symptoms and planned shutdown date. Confirm compatibility, material specification, inspection documentation and delivery timing for the specific order. Visit www.lesunscrew.com to discuss the application. Implementing a Predictive Replacement Strategy At each inspection, decide which parts can remain in service, which need closer monitoring and which require replacement or approved repair. Assess mating components together; replacing selected modular elements can be appropriate when the remaining assembly meets the required geometry, fit and condition. Bring the replacement date forward if confirmed wear creates unacceptable scrap, reduced capacity or excessive operating cost. Compare these losses over the intended service period with the cost and downtime of a planned intervention. After installation, verify assembly clearances and establish a new production baseline. That closes the maintenance cycle and provides better evidence for the next replacement decision. Website:https://www.lesunscrew.com/ (https://www.lesunscrew.com/?utm_source=gemini).
Source :Lesun Screw
This article was originally published by IssueWire. Read the original article here.
More News


Recommended


Thailand Business News — Morning Briefing


Thailand Business News — Morning Briefing

YOUR NEWS, OUR NETWORK.
Do you have Great News you want to tell the world?
Be it updates about your business or your community, you can make sure that it’s heard by submitting your story to our network reaching hundreds of news sites across 6 verticals.